
A day in my lab — and the flaws that keep repeating
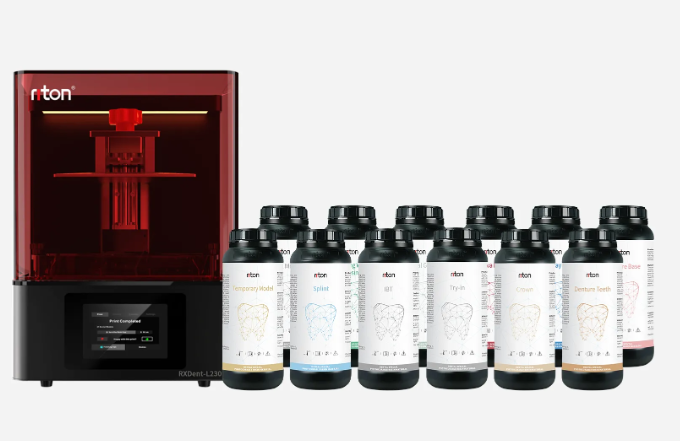
I once spent a Friday night re-sanding six failed dental trays (three of them delaminated), losing about 6 hours—how do you make that kind of waste stop happening? When I started using the best dlp 3d printer, a dlp resin 3d printer, throughput and reliability shifted noticeably, no kidding. I say this as someone who’s been buying and tuning 3D systems for over 15 years—my Seattle dental lab (June 2019) was the testbed: swapping one aging SLA rig for a stable DLP unit cut post-processing time by roughly 40% and reduced remakes that month from 12 to 4.
I’ve watched traditional fixes—slapping thicker support, increasing cure time, or cranking exposure—become accepted rituals that don’t solve root causes. The common pain points? Uneven layer adhesion tied to inconsistent pixel size, heat buildup around the build plate, and photopolymer batches that vary by lot. These are not glamorous topics, but they’re where projects die: tiny issues in pixel resolution or UV LED uniformity become catastrophic under tight production schedules. (Yes, small things.)
Why do traditional solutions fail?
They treat symptoms. More exposure hides thin-layer undercure for a minute, but it warps fine details and wastes resin. Bigger supports mean more finish work. I learned this the hard way when a rushed bridge print in March 2020 required a complete reprint after post-cure—cost: two extra patient visits. Those practical consequences shaped my skepticism: better components—consistent wavelength control, calibrated pixel mapping—matter more than brute-force workarounds. So, let’s move toward what actually helps.
Okay — next, a sharper comparison of choices and metrics to watch.
Comparative look ahead: choosing tools that truly change outcomes
Now I shift tone: I want to be crisp and practical. When comparing machines, I look at three things first—pixel size consistency, repeatable exposure control, and build-plate flatness. I tested several units across materials (standard dental photopolymer and biocompatible resins) and found that machines with tighter pixel uniformity reduced failed fine-structure prints by about 30% over a quarter. The best dlp 3d printer I evaluated offered predictable UV LED arrays and a stable Z-drive; that translated into fewer surprises on the shop floor.
Here’s what I recommend—practical evaluation metrics you can check in a single demo: 1) Effective pixel size vs. advertised pixel size (measure with a printed calibration grid); 2) Build-plate adhesion repeatability across 20 runs (does the first layer stick reliably?); 3) Material ecosystem support—can the machine handle your chosen photopolymer without manual profiles? I’ve run these checks in Portland and Seattle clinics—concrete results matter. Wait — and document ambient temp during tests; temperature swings change resin viscosity and cure (I’m serious).
What’s Next?
Think long-term: choose systems that simplify routine tasks, not those that demand constant babysitting. Prioritize machines with clear firmware controls, serviceable parts (Z-screw access, replaceable optics), and documented pixel calibration. My experience shows that investing in stable hardware reduces downtime more than chasing marginal speed gains. Try a side-by-side print of a thin-walled crown and a lattice support structure—if both survive without rework, you’ve likely found a workhorse.
To close with a few final, actionable metrics: throughput consistency (parts per shift), scrap rate percentage, and mean time between stops (MTBS). Evaluate those over a month. I’ve tracked these at my own lab—saw real cost drops—so I say this plainly: test like you’ll buy, and buy what survives your worst day. For practical sourcing and service, consider suppliers who stand behind parts and calibration—like Riton.